 Technical
Refined Cotton vs. Wood Pulp in Cellulose Derivatives
Degree of polymerization, reactivity and cost compared — and the processes where cotton-based cellulose is not optional.
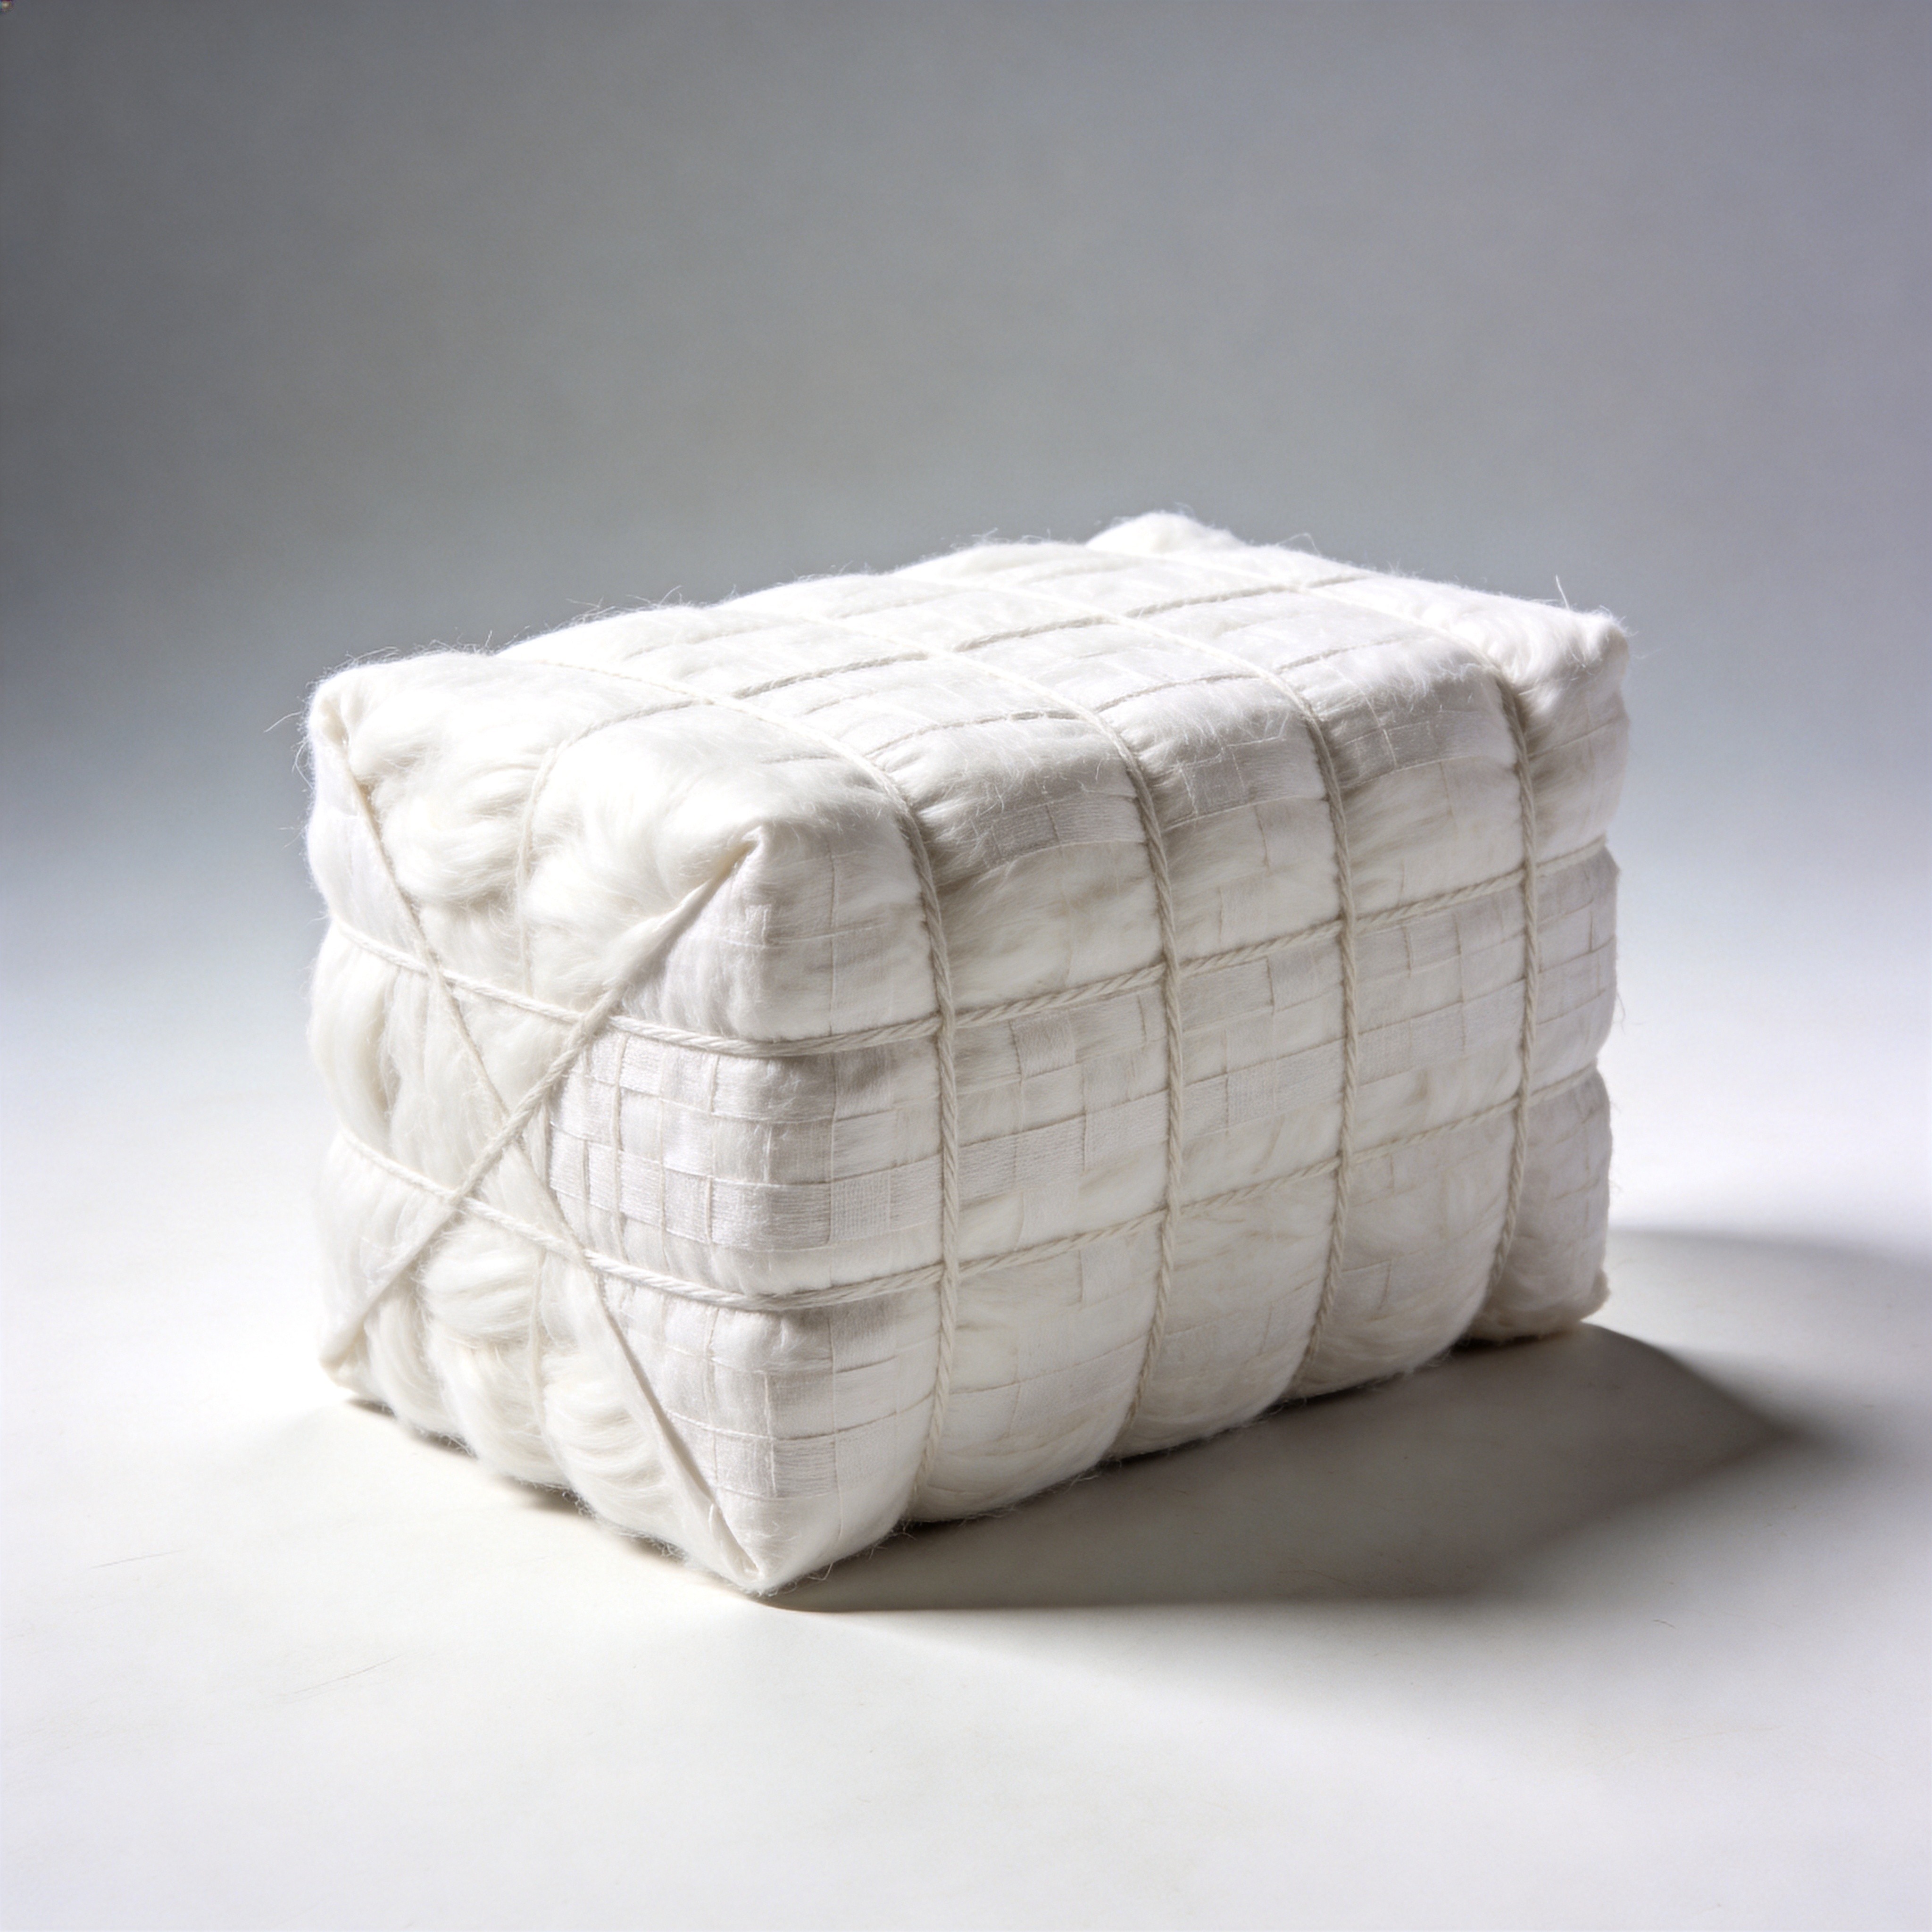
Read More →When buyers ask for "a refined cotton quote," the first question from our side is always the same: what is your target viscosity? Viscosity grade is the single most influential property of refined cotton for downstream production. It reflects the average chain length of the cellulose molecules, and it sets reaction kinetics, reagent consumption and the performance ceiling of the finished derivative — whether that is HPMC ether, nitrocellulose, cellulose acetate or microcrystalline cellulose. This guide explains how viscosity grades are typically grouped, what each group does in a reactor, and how α-cellulose, ash and iron change the picture.
Refined cotton is almost pure cellulose. Its molecules are long chains of glucose units; the average number of units per chain is the degree of polymerization, or DP. Longer chains make more viscous solutions after dissolution or derivatization, while shorter chains give low-viscosity, fast-reacting material. Commercial grade codes commonly encode this — for example, an "M200" grade names a product family (M) and a viscosity level (200), with the full M5 to M1000 range covering low to high viscosity needs.
Two producers offering "the same" number can still behave differently in your reactor. Test method matters: viscosity is usually measured on a cuprammonium or cupriethylenediamine (CUEN/CED) solution at fixed concentration and temperature. Always compare quotes against the same method, and ask the mill for the actual measured range rather than a nominal value.
A common misunderstanding is treating viscosity as a quality mark — higher is better. It is not. Viscosity describes chain length distribution; purity is described by α-cellulose, ash and iron. A high-viscosity grade can be poorly purified, and a low-viscosity grade can be extremely clean. In your plant, chain length controls three things:
Low-viscosity refined cotton (roughly the M5 to M60 band) consists of shorter cellulose chains. It is the workhorse for low-viscosity ether grades used in applications such as construction admixtures and detergent polymers, where builders need good solution workability rather than thickening power, and for derivatization processes that must complete quickly and uniformly in continuous or short-cycle reactors.
The risk at the low end is over-depolymerization: if the chain-length distribution is too broad or the average is cut too far, substitution becomes uneven and yield drops. Reputable mills control the cooking and bleaching stages to hold a stable viscosity window rather than simply hitting a maximum.
The medium band (roughly M100 to M400) is where most cellulose ether production lives. HPMC and HEMC makers building construction-grade water retention agents, as well as many HEC and CMC producers, specify this range because it balances two competing needs: enough chain length for meaningful thickening and water retention in the finished product, and enough reactivity to complete etherification within practical cycle times.
Within this band, selection is usually made together with α-cellulose. Etherification is a diffusion-driven reaction: reagents must penetrate the swollen fiber uniformly. High α-cellulose feedstock — meaning little residual hemicellulose and lignin — reacts more evenly and leaves fewer unreacted zones, which shows up as cleaner solution clarity and fewer gel particles. Many buyers lock two numbers in their specification: a viscosity window and an α-cellulose minimum.
High-viscosity grades (roughly M650 to M1000) preserve long cellulose chains and serve applications where the polymer backbone is the performance feature: high-viscosity ethers for premium thickening, certain nitrocellulose grades used in coatings and inks, and specialty ester or film uses requiring mechanical strength. In these processes, feedstock variability hurts more — a shift in incoming DP changes product viscosity far outside the finished-goods tolerance.
Because high-DP cellulose reacts more slowly, process teams typically extend alkali steeping and etherification times and watch reagent ratios more carefully. Specifying a mill with batch-consistent viscosity control matters more here than chasing a peak number; a grade that runs identically shipment after shipment is worth more than a higher nominal value that drifts.

Cellulose pulp contains three fractions. The α-fraction is the true, high-molecular cellulose; β and γ fractions are shorter hemicellulosic material. α-Cellulose content measures how much of the product is the reactive, stable component. Hemicellulose consumes etherifying and esterifying reagents without contributing to target polymer properties, promotes side reactions, and can raise ash and color. In practice, high-grade refined cotton runs at high α-cellulose levels — leading grades sit above 98% — while lower numbers are acceptable only in cost-sensitive, low-spec end uses. Buyers should read the α-cellulose figure off the TDS and verify it on the batch COA rather than assuming it.
Ash is the inorganic residue left after burning a sample — metal ions, salts and dust carried in from water, processing equipment or incomplete washing. Iron is tracked separately because of what it does chemically. Transition metal ions, iron above all, catalyze oxidation and degrade cellulose during high-temperature processing and long storage; in nitrocellulose they affect stability and color, and in film and acetate uses they show up as haze or discoloration.
Ash is commonly well below 1% on good refined cotton, but the important targets are the tight ones: specialty and nitrocellulose grades often require iron in the low ppm range. These figures cannot be corrected later in your plant — they are fixed at the mill's washing and water-treatment stages. If your end product is color- or stability-sensitive, write ash and iron limits into the specification from the first sample order.
A good inquiry answers five questions and removes a full round of guessing:
With those five points, a technical sales team can name a grade from the M / X / C series, send the matching TDS, and ship sample material with a batch COA for line trials. Grade selection is rarely a one-shot decision: it is normal to test two neighboring viscosity levels in parallel and settle on the one your reactor prefers. That is exactly what sample orders are for.
TechnicalDegree of polymerization, reactivity and cost compared — and the processes where cotton-based cellulose is not optional.
Read More → Technical
The meaning of the α-fraction, how hemicellulose wastes reagents, and the number to check on every TDS.
Read More →Our technical team answers within 24 work hours — send your target viscosity, α-cellulose minimum and any ash/iron limits, and we will match a grade and ship sample material with a batch COA.
● WhatsApp usually answered within 1 hour on workdays (GMT+8)